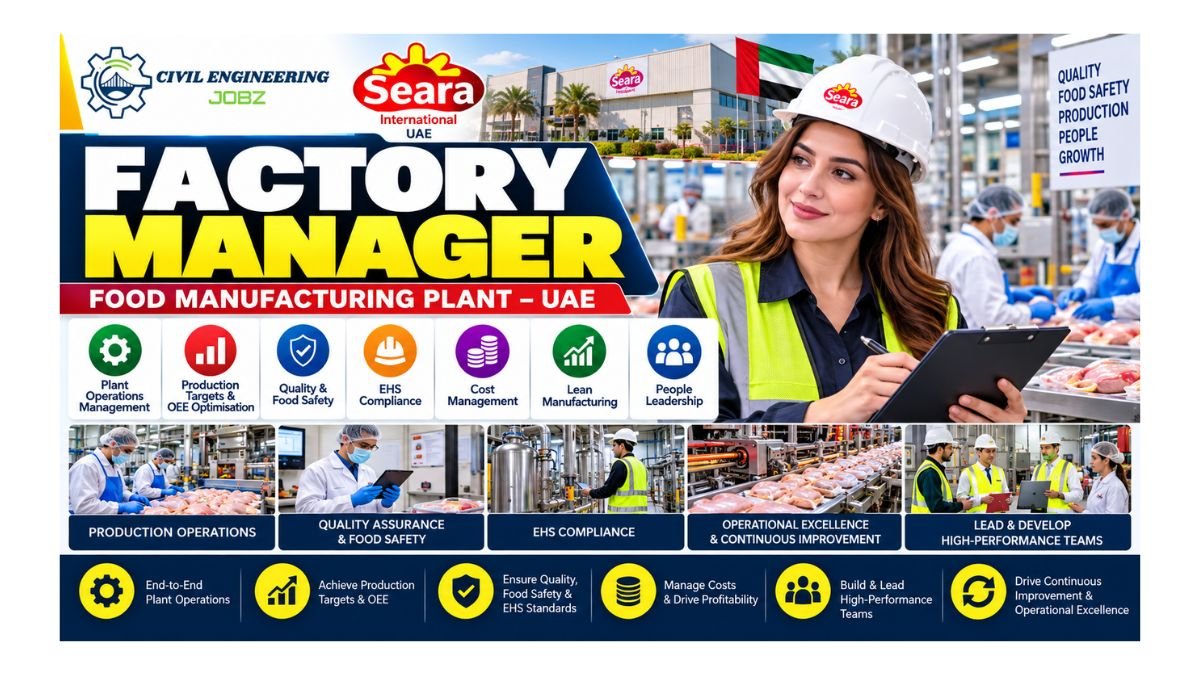
Seara International UAE is hiring a highly experienced and results-driven Factory Manager to provide strategic and operational leadership across its UAE manufacturing plant. This is a senior executive role with full end-to-end responsibility for plant operations, production targets, quality, food safety, EHS compliance, cost management, OEE optimisation, Lean Manufacturing, and people leadership. The ideal candidate brings 15+ years of manufacturing experience, 10+ years in plant or senior operations management, and a proven track record in operational excellence, continuous improvement, and building high-performance manufacturing teams in food, FMCG, poultry, meat processing, or frozen food environments.
About Seara International — UAE
Company: Seara International — a globally recognised food brand operating in the UAE and broader MENA region
Products: Poultry, meat processing, frozen foods, and protein products for retail, foodservice, and export markets
Standards: World-class food safety, quality, EHS, Lean Manufacturing, and operational excellence standards
🇦🇪 UAE Operations: Manufacturing facility serving the UAE, GCC, and regional markets
Culture: Performance-driven, compliance-focused, and dedicated to building great teams and manufacturing capabilities
Operational Excellence Framework You Will Lead
Lean Manufacturing: Waste elimination, value stream mapping, flow optimisation, and pull systems across the plant
Six Sigma: Data-driven defect reduction, DMAIC methodology, statistical process control, and variation reduction
OEE (Overall Equipment Effectiveness): Availability, performance, and quality rate optimisation across all production assets
TPM: Total Productive Maintenance and equipment reliability to maximise uptime and asset utilisation
Continuous Improvement: Kaizen, PDCA, root cause analysis, and loss reduction across all plant functions
Why This Factory Manager Role at Seara International UAE Stands Out: This is one of the most senior and comprehensive plant leadership positions available in the UAE’s FMCG and food manufacturing sector in 2026. You will have full end-to-end accountability for plant operations — from production planning and cost management through to Lean transformation, capital investment input, and building the next generation of manufacturing leaders. For a seasoned factory or plant manager looking for a senior executive manufacturing leadership role in the UAE with global brand backing and genuine operational scope, this Seara International opportunity is exceptional.
Position Overview
As Factory Manager at Seara International UAE, you will be the senior operational leader of the manufacturing facility — holding full accountability for achieving production, quality, service, productivity, and cost targets while maximising asset utilisation and ensuring full compliance with safety, food safety, quality, environmental, and statutory requirements. You will develop and execute the annual Business Plan, lead Lean Manufacturing and Six Sigma continuous improvement programmes, oversee new equipment and process implementations, provide input for capital investment decisions, and — critically — assess, develop, and coach your team and future leaders to build long-term organisational capability. This is a strategic, high-accountability role that demands a manufacturing leader of significant experience, credibility, and operational breadth.
Key Responsibilities
Plant Operations & Performance Management
- Lead plant operations to achieve production, quality, service, productivity, and cost targets — holding full accountability for all aspects of factory performance and driving a high-performance operational culture across every shift and function.
- Develop and execute the annual Business Plan (BP) aligned with company objectives and strategic priorities — translating company strategy into operational plans, budgets, KPI frameworks, and team-level objectives for the manufacturing facility.
- Review plant performance daily, weekly, and monthly — ensuring timely corrective actions are taken when performance deviates from plan and that improvements are sustainable, data-driven, and properly communicated.
- Maximise asset utilisation, labour productivity, capacity, and operational efficiency — applying rigorous OEE principles, workforce planning, and process improvement methodologies to extract maximum value from the plant’s assets and people.
Lean, Continuous Improvement & Projects
- Drive Lean Manufacturing, Six Sigma, problem-solving, and continuous improvement initiatives — leading the factory’s CI programme to systematically reduce losses, waste, and costs while improving quality, throughput, and reliability.
- Lead the implementation of new equipment, products, processes, projects, and capacity expansions — from business case development through to successful commissioning and handover to the operational team.
- Provide input for infrastructure development, plant layout, and capital investment requirements — applying operational expertise to ensure that future investments deliver the intended capacity, efficiency, and quality improvements.
Safety, Compliance & Food Safety
- Ensure full compliance with safety, food safety, quality, environmental, and statutory requirements — maintaining a zero-compromise approach to EHS, GMP, HACCP, and regulatory compliance across all plant operations at all times.
- Ensure finished goods availability in plant warehouses according to production plans and market requirements — managing the link between production, warehousing, and commercial functions to achieve on-time-in-full (OTIF) performance.
People Leadership & Organisational Development
- Assess organisational structure, staffing, and competency needs — building the right team for current and future operational requirements, identifying capability gaps, and developing structured development plans for all key roles.
- Develop, coach, and build future leaders — investing in the growth of direct reports and high-potential talent to build deep organisational capability and succession pipeline within the manufacturing function.
- Establish accountability through clear objectives, performance appraisals, and effective performance management — creating a culture where everyone understands their targets, receives regular feedback, and is held to consistent standards.
Qualifications & Requirements
- Bachelor’s degree in Engineering, Food Science, Manufacturing, or a related field — with an MBA as an additional advantage for managing the strategic and financial dimensions of plant leadership at this level.
- Minimum 15+ years of manufacturing experience, including 10+ years in plant or senior operations management — this is a firm experience threshold reflecting the seniority and complexity of this factory leadership role.
- Experience in food manufacturing, poultry, meat processing, frozen foods, or FMCG is strongly preferred — direct sector knowledge accelerates impact in regulated, quality-critical food production environments.
- Proven track record in operational excellence, cost optimisation, productivity improvement, and people leadership — demonstrable results across multiple manufacturing KPIs, with a history of sustainable performance improvement.
- Strong knowledge of Lean Manufacturing, continuous improvement, food safety, quality management, and EHS standards — applied hands-on expertise, not just theoretical knowledge.
- Strong analytical, financial, problem-solving, communication, and change management skills — the Factory Manager operates at the intersection of operational detail and strategic business leadership.
Who Should Apply?
- Senior Factory / Plant Managers in the UAE or GCC: With 15+ years manufacturing experience, 10+ years in plant leadership, and a track record of operational excellence in food, FMCG, poultry, or meat processing environments.
- Operational Excellence Leaders: Manufacturing managers with deep Lean, Six Sigma, OEE, and continuous improvement expertise — who have delivered measurable, sustainable cost and efficiency improvements at plant level.
- Food Industry Manufacturing Directors: Senior professionals from food manufacturing, poultry processing, frozen foods, or FMCG looking for a Factory Manager role with full plant ownership at a globally respected food brand in the UAE.
- People-First Manufacturing Leaders: Factory managers who combine technical operational expertise with genuine people leadership capability — building teams, coaching future leaders, and creating accountability-driven manufacturing cultures.
- MBA-Qualified Manufacturing Professionals: Engineering or food science graduates with an MBA and demonstrated ability to link plant-level operations to strategic business objectives, financial performance, and cross-functional collaboration.
Recently Opening Jobs👇